


Raising a glass to resource efficiency, quality, and reliability
Innovation in the beverage world doesn’t stand still — and neither do we. So, whether you're brewing, bottling, blending, or breaking into a new category, we’re proud to help turn those ideas into standout products — not just once, but again and again.
GEA technologies could help you reduce waste, recycle energy and water, and cut carbon footprint, whether you’re looking to upgrade an existing site, or build from the ground up. And of course, hygienic design is central to all of our equipment, from dealcoholization units and pasteurization plants, to CO₂ recovery systems and homogenizers.
Dedicated technology and test centers
Our global network of beverage technology and test centers of excellence comprise purpose-built hubs, packed with GEA equipment, where you can work with our experts to test, tweak, scale up and problem solve.
We’ll use our know-how and decades of experience collaborating with customers around the word to help you overcome production puzzles, improve resource efficiency, and scale effectively. With our support and know-how you’ll be better equipped to bring high-quality alcoholic and non-alcoholic drinks to market with fewer delays.
Our labs and pilot-scale environments offer:


Solutions for excellence in competitive markets
We don’t just provide equipment — we engineer confidence. Our focus is on creating solutions to keep you competitive in fast-moving markets, whether you’re refreshing a classic or breaking ground with a something new.
We’ll take the time to learn about your mineral water, plant-based drink or a malt-based beverage, so we can better understand your goals, challenges and budgets. We’ll then sit with you to tailor individual components, stand-alone skids, or integrated systems and end-to-end lines that best fit with your processes, products and physical setup.
Smart solutions for every format and formulation
Behind every successful beverage is the right blend of innovation and reliability. GEA’s smart solutions cover the full production spectrum, and are designed to integrate smoothly and scale effortlessly, whatever your format or formulation.
We’ve also spent decades developing user-friendly automation and process control software that keeps your production at peak performance. Our cloud-based plant monitoring and optimization platform maintains minute-by-minute oversight of your plant’s operation and can even adjust key process parameters to ensure peak performance and efficiency with minimal manual intervention.
Beverage processing in action
Discover how beverage producers are driving innovation with GEA.
Explore real-world success stories from beverage manufacturers around the world. See how leading brands are partnering with GEA to overcome production challenges, improve efficiency, and bring innovative drinks to market – all powered by advanced process technology and smart solutions.


Pokka
GEA ABF produces LA aseptic beverages at Pokka


Bushmills
GEA partner with Bushmills to build an extension to their distillery, increasing their yield while also improving their carbon footprint


GEA Beverage on LinkedIn
A thirst for the extraordinary
Products & Technologies
Showing 4 of 75

Ancillary Equipment
Ancillary equipment for centrifuges contributes to more sustainable production by making utilities reusable, saving energy and increasing the overall process efficiency.

Aseptic Systems
Here at GEA, we’ve developed a range of aseptic systems for liquid processing that are designed to give you confidence in maintaining sterile conditions throughout the production process and during storage. Relied on by our global customers in food, beverage, dairy and pharmaceuticals manufacturing, GEA aseptic equipment is engineered so you can ...

Aseptic valves & components
Aseptic valves face exceptionally high demands within UltraClean and Aseptic processes. You can be assured that they all provide highest quality in terms of hygienic design and sustainability.

Automatic Powder Fillers
Our Inline Automatic Filler range has been designed to provide a flexible powder filling solution to suit plants which may need to increase production capacity to meet future demand.
The Inline Filler range comprises a single head model (IBF-450) that can be upgraded to include a single top-up system (IBF-600) or dual top-up system (IBF-800) to ...
Downloads
Related Videos
A day of celebration: 150 years brewing systems at GEA
Ariete Homogenizer 5400 - the highest performance homogenizer in the world
GEA Control valves - TEFASEP® gold and RVIN guarantee long lifetime of the product
GEA Insights
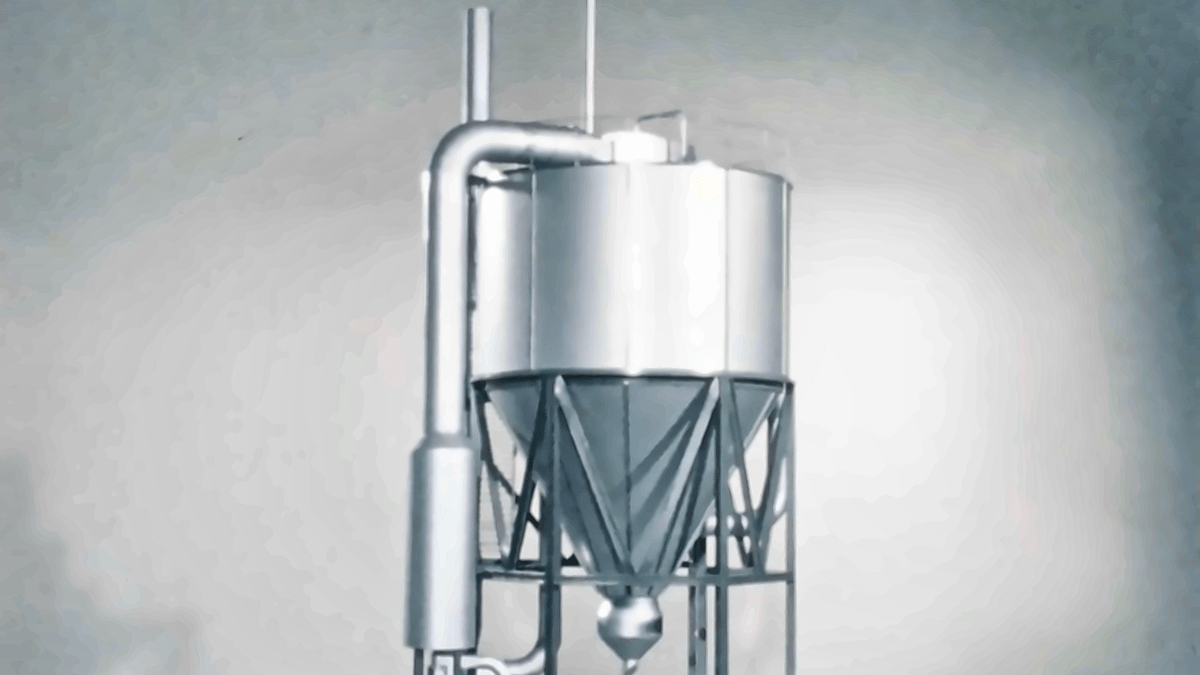
The breakthrough that changed spray drying
In 1976, NIRO engineers responded to a competitive challenge by rethinking what spray drying could do. Their idea became the multi-stage dryer MSD. Fifty years later, the same fundamental principle helps turn liquids into the powders used in essential nutrition products and important medicines around the world. Refined through decades of engineering expertise, customer insight and continuous development, MSD is a story of innovation with lasting impact.
Beyond the machine: unlocking better plant performance
An efficient machine does not automatically make an efficient factory. Real improvement often starts by looking beyond individual equipment and understanding how processes, energy systems and operating decisions affect one another. It’s a holistic approach designed to uncover opportunities that might otherwise be missed.
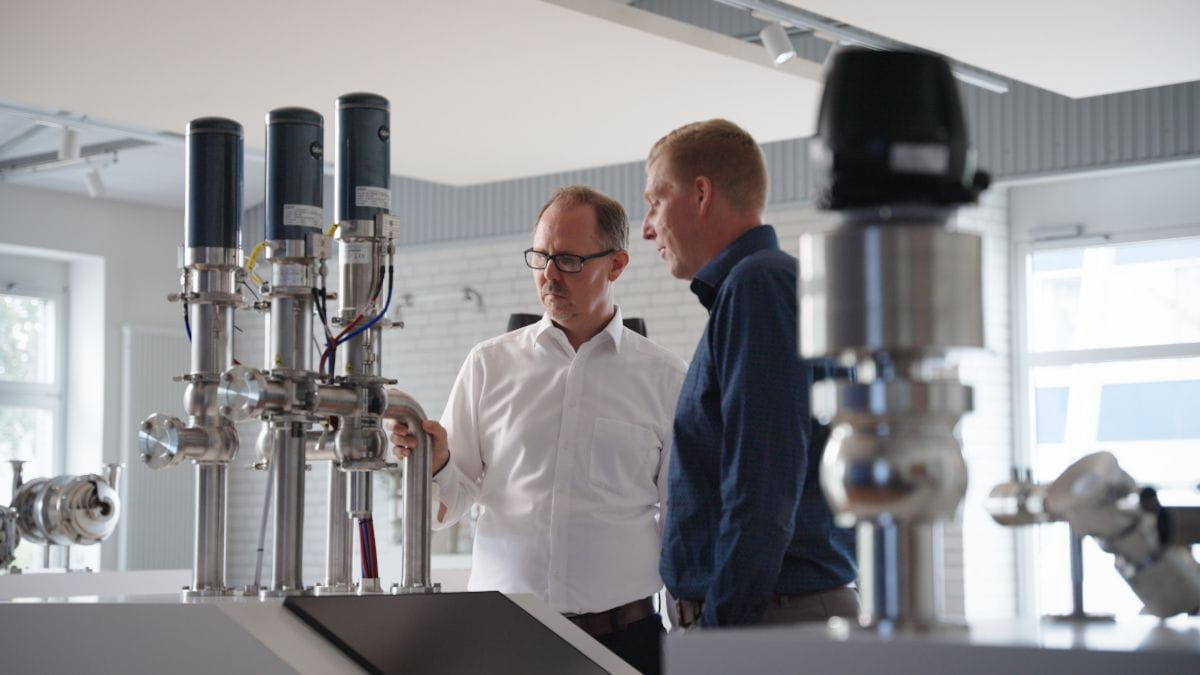
How a valve reshapes the way food and drinks are made
In food and beverage plants, valves are commonly operated using compressed air. GEA Hydract® Actuation Technology moves valves with water instead, in a closed, digitally controlled circuit. The result is a valve that can be held exactly in place and steered in fine-tuned steps. This results in lower energy use and greater control.
